Titanium rolling transforms cast ingots or billets into sheet, strip, and plate through controlled deformation. Hot rolling, performed above ~800°C in the α+β phase field (or above the beta transus for opening passes), is the primary method for producing plate and thick sheet. Cold rolling, done at room temperature with reductions limited to 10–20% per pass before intermediate annealing, produces precision thin sheet and foil with superior surface finish and tighter tolerances. A third option — warm rolling at 500–700°C — bridges the gap for applications needing better surface quality than hot rolling with less work hardening than cold rolling. The governing standard for titanium sheet in the US is ASTM B265; aerospace sheet is typically qualified under AMS 4911 (Ti-6Al-4V). Choosing the right rolling method depends on alloy grade, target thickness, required mechanical properties, and surface finish.
Why Titanium Rolling Is Different From Rolling Steel
Most engineers who’ve worked with steel rolling transfer those mental models to titanium — and run into problems immediately.
Titanium is not forgiving. The plastic working window is narrow. Go too cold and edge cracks develop; go too hot above the beta transus and beta grains grow rapidly, locking in a coarse Widmanstätten microstructure that compromises room-temperature ductility and fatigue life. The alloy is reactive at elevated temperature, picking up oxygen and nitrogen from furnace atmospheres to form a brittle surface layer called alpha case — invisible to the eye but catastrophically damaging to fatigue performance.
Three properties drive these differences:
- High strength at elevated temperature. Ti-6Al-4V still has a yield strength above 400 MPa at 700°C. Rolling forces are substantially higher than equivalent steel operations.
- Narrow recrystallization window. For CP Grade 2, recrystallization annealing typically occurs at 650–760°C. For Ti-6Al-4V, it is 700–845°C. Staying in range requires accurate furnace control.
- Phase transformation sensitivity. The beta transus (the temperature above which the microstructure is entirely BCC β phase) varies by alloy and directly controls what rolling regime you’re in. For Ti-6Al-4V this is approximately 995°C; for CP Grade 2, approximately 882°C. Rolling above or below this boundary produces fundamentally different microstructures.
Understanding these three factors is the foundation for all of what follows.
The Three Rolling Regimes for Titanium
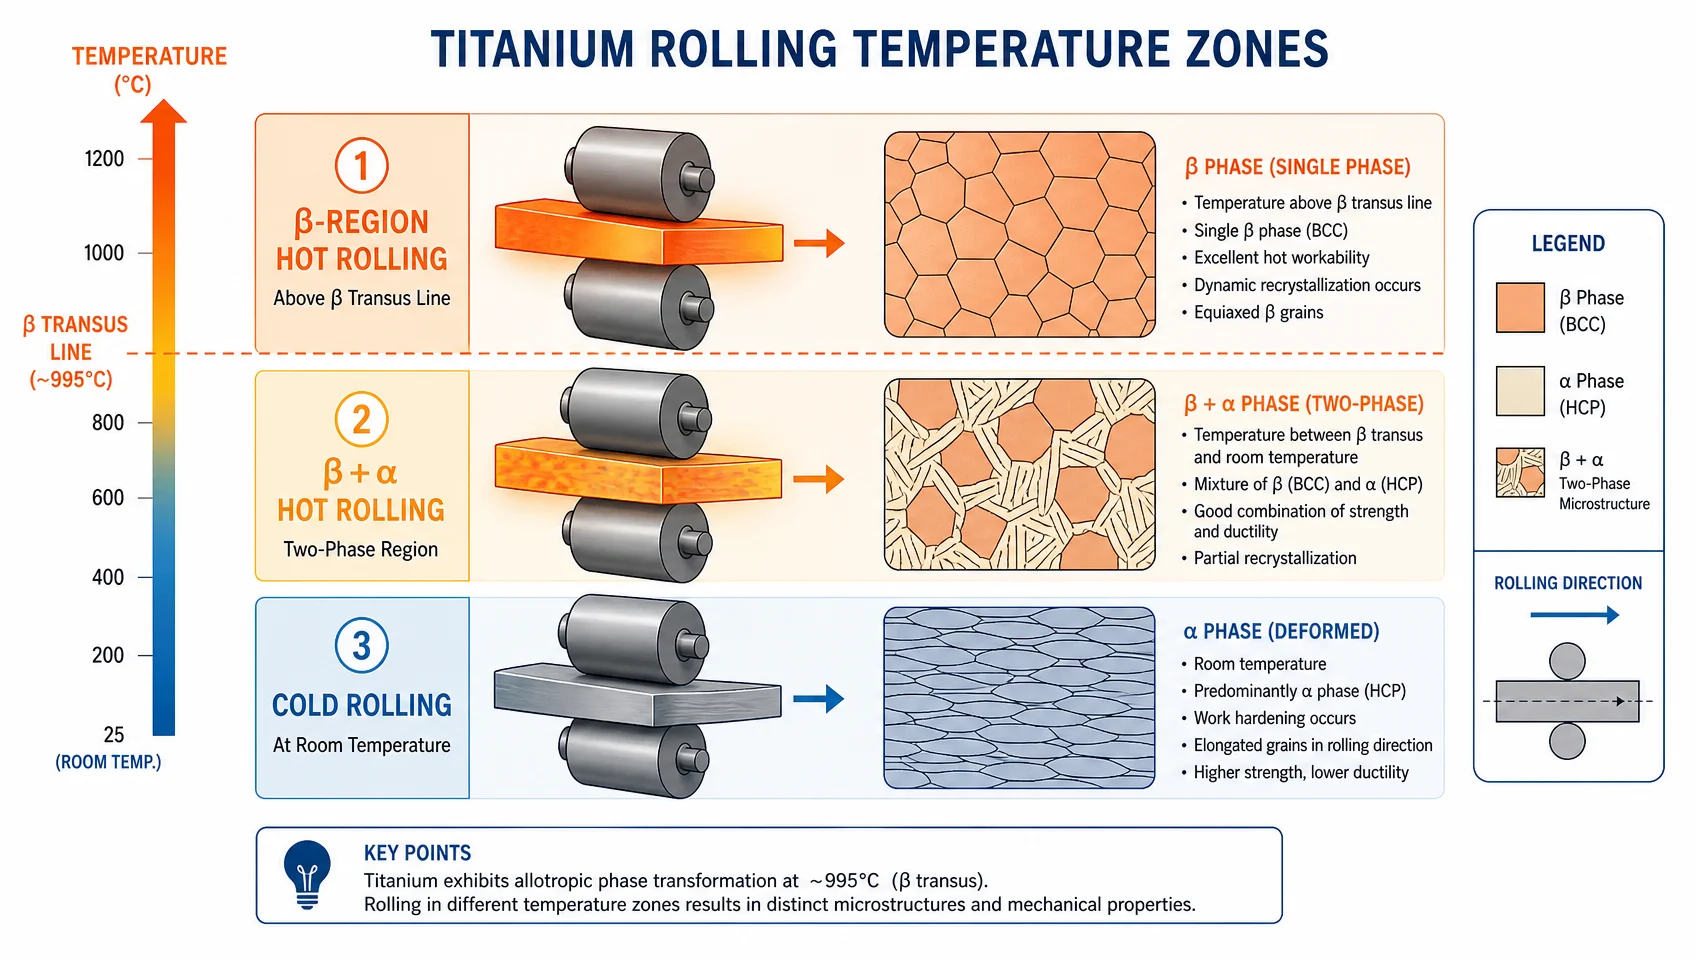
Titanium sheet production uses three distinct thermal regimes, not two. Most commercial content ignores warm rolling, which is a mistake — it is the preferred option for several product categories.
Hot Rolling (Above ~800°C, in the α+β Region)
This is the workhorse process for titanium plate and thick sheet. It breaks up the coarse, porous cast structure of the billet, refines grain size, and achieves the large thickness reductions needed to get from slab to usable gauge.
Two sub-regimes exist within hot rolling:
β-region rolling is performed 150–250°C above the beta transus. In this regime deformation resistance is low and large reductions are possible per pass. The trade-off is rapid β grain growth, which produces coarse Widmanstätten or “basketweave” α structures on cooling — acceptable for high-temperature creep applications but poor for room-temperature fatigue-critical parts. β-region rolling is primarily used for billet opening and intermediate breakdown, not for final sheet production.
(α+β) region rolling, conducted 20–200°C below the beta transus, is where final plate and sheet reduction happens. Primary α and β phases coexist in this window. Deformation breaks up and refines the microstructure. The α phase elongates along the rolling direction, and if sufficient cross-rolling or bidirectional rolling is applied, a fine equiaxed or dual-phase microstructure develops — the basis for titanium sheet with high strength, good ductility, and fatigue resistance simultaneously.
Hot rolling temperature windows by alloy (starting temperature, °C):
| Alloy | Beta Transus (°C) | β-Region Rolling | (α+β) Region Rolling |
|---|---|---|---|
| CP Grade 1 | ~882 | 1000–1050 | 750–870 |
| CP Grade 2 | ~882 | 1000–1050 | 750–870 |
| CP Grade 3 | ~900 | 1020–1070 | 800–890 |
| CP Grade 4 | ~950 | 1060–1110 | 850–940 |
| Ti-3Al-2.5V | ~935 | 1060–1110 | 840–920 |
| Ti-6Al-4V | ~995 | 1100–1150 | 850–980 |
Note: Start temperatures vary by slab thickness, mill capability, and target microstructure. Finish rolling temperature (the temperature at the last pass) is the critical control variable — typically ≥800°C for CP grades and ≥850°C for Ti-6Al-4V to avoid uncontrolled deformation in a largely α microstructure.
Reduction per pass in hot rolling: Typical pass reductions run 15–30% for (α+β) region rolling. β-region billet breaking can achieve 30–40% per pass. Total hot reduction from slab to final hot-band thickness can exceed 80%.
Surface condition after hot rolling: Oxide scale forms readily above ~600°C. After hot rolling, sheet requires pickling in HF-HNO₃ solution (typically 2–5% HF + 15–30% HNO₃) to remove scale and any alpha case layer. Without complete scale and alpha case removal, cold rolling will embed surface contamination into the sheet.
Cold Rolling (Room Temperature)
Cold rolling of titanium is not a high-speed, continuous process like cold rolling steel strip. Titanium work-hardens rapidly at room temperature, and ductility drops sharply after even modest cold work.
The governing constraints:
- Reduction per pass: 5–15% is typical; 20% is near the practical limit for most titanium alloys without cracking or excessive mill load. This is two to four times lower than cold rolling of austenitic stainless steel.
- Total cold work before intermediate anneal: Generally limited to 30–60% total reduction, depending on alloy. CP Grade 1 can tolerate more cold work than Ti-6Al-4V before annealing is mandatory.
- Intermediate annealing is required after each 30–60% total reduction cycle. For CP grades, anneal at 650–760°C for 30–60 minutes, furnace cool or air cool. For Ti-6Al-4V, anneal at 700–790°C for 1–4 hours depending on section thickness.
What cold rolling achieves that hot rolling cannot:
- Dimensional tolerance. Hot-rolled titanium sheet has thickness tolerances per ASTM B265 of ±0.33 mm or more at 3 mm thickness. Cold-rolled sheet can hold ±0.05–0.10 mm at the same gauge.
- Surface finish. Hot-rolled and pickled sheet typically achieves Ra 1.6–6.3 µm. Cold-rolled sheet reaches Ra 0.4–1.6 µm, and bright-annealed cold-rolled foil can reach Ra <0.2 µm.
- Increased yield strength. Cold work increases yield strength through dislocation accumulation. A Ti-6Al-4V sheet with 30% cold work can show a 15–25% increase in yield strength vs fully annealed condition — useful for spring-back compensation in formed parts.
Applications exclusive to cold rolling: Titanium foil (<0.1 mm), precision shim stock, thin wall heat exchanger tubing strip, and any application requiring surface finish Ra < 1.6 µm.
Warm Rolling (500–700°C) — The Overlooked Middle Option
Warm rolling is performed above the recovery temperature but below full recrystallization. For titanium, this typically means 500–700°C.
At these temperatures:
- Deformation resistance is reduced compared to room temperature (smaller rolling forces, less risk of edge cracking)
- Oxidation is lower than hot rolling, producing a thinner, more manageable scale
- Dimensional control is better than hot rolling
- Grain refinement occurs through dynamic recovery, not full recrystallization — producing a finer, more uniform microstructure than cold rolling alone
When warm rolling makes sense:
- Producing titanium foil or thin strip where multiple cold rolling + annealing cycles are cost-prohibitive
- Ti-3Al-2.5V tubing strip (this alloy is commonly produced via warm rolling)
- Situations where hot-rolled surface quality is unacceptable but full cold rolling infrastructure is unavailable
- As an intermediate step between hot and cold rolling to improve homogeneity before final cold passes
Head-to-Head: Hot Rolling vs Cold Rolling for Titanium
| Parameter | Hot Rolling | Cold Rolling |
|---|---|---|
| Temperature | 800–1150°C (alloy dependent) | Room temperature |
| Reduction per pass | 15–30% | 5–15% (max ~20%) |
| Total reduction achievable | >80% from slab | 30–60% before anneal |
| Surface finish (Ra) | 1.6–6.3 µm after pickle | 0.4–1.6 µm |
| Dimensional tolerance | ±0.25–0.50 mm typical | ±0.05–0.15 mm |
| Microstructure control | Grain refinement via thermo-mechanical control | Work hardening; must anneal to restore ductility |
| Oxidation/alpha case | Significant; mandatory pickling | None (room temp) |
| Lubrication | Scale/oxide acts as lubricant; protective coatings for Ti-Al alloys | Synthetic rolling oils required; titanium cannot use sulfurized lubricants |
| Minimum achievable thickness | ~0.5–1.0 mm practical limit | <0.025 mm (foil) |
| Cost | Lower per pass; high energy | Higher total cost (multiple passes + anneals) |
| Typical ASTM B265 condition | Annealed (Condition A) | Annealed (A), cold-worked stress-relieved ©, or as-rolled |
Understanding ASTM B265 Conditions
ASTM B265 — the primary specification for titanium strip, sheet, and plate in the US — covers material in these conditions:
- Condition A (Annealed): Material that has been annealed after final rolling. This is the most common condition for aerospace, chemical, and general industrial use. It provides maximum ductility and the lowest residual stress.
- Condition C (Cold Worked and Stress Relieved): Cold-rolled material that has been stress-relieved but not fully annealed. Higher yield strength than Condition A; reduced elongation.
- Condition STA (Solution Treated and Aged): For alpha-beta alloys like Ti-6Al-4V. Achieves maximum strength. Not produced by rolling alone — requires solution treatment and aging heat treatment after rolling.
For most procurement engineers: if you need formability, specify Condition A. If you need higher yield strength and are willing to accept lower elongation, ask your supplier about Condition C.
Alpha Case: The Rolling Defect Nobody Talks About Enough
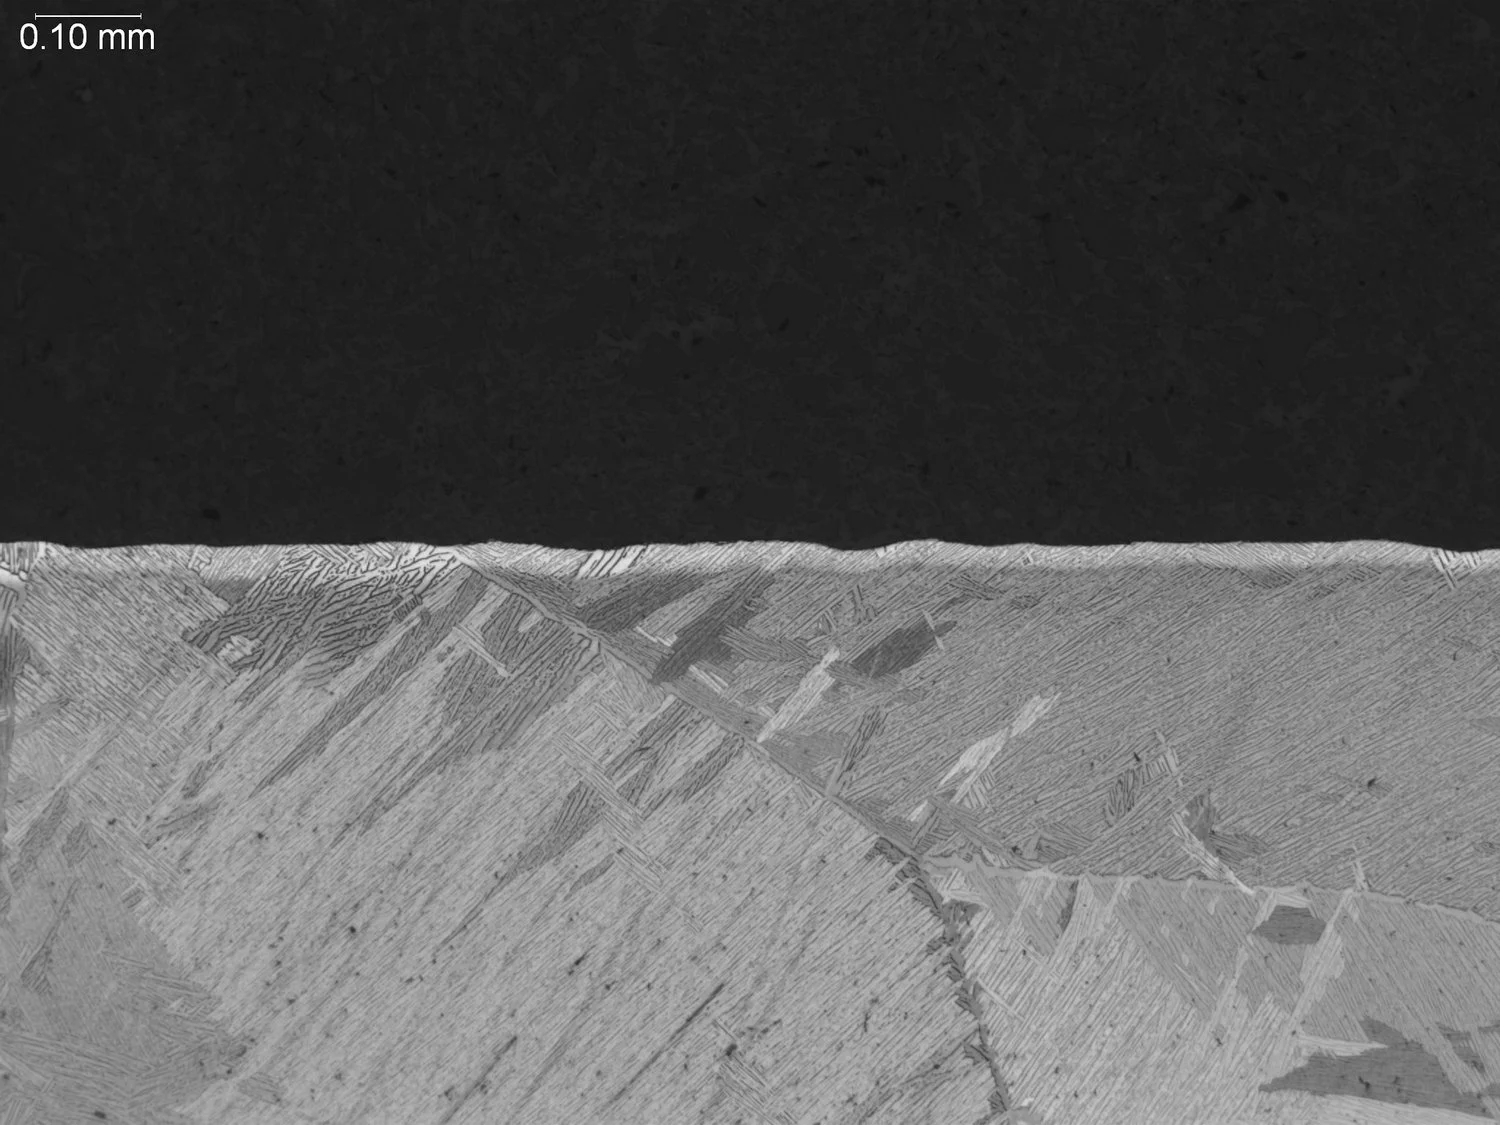
Alpha case is a surface zone of elevated oxygen content that forms when titanium is heated above ~600°C in air or in an oxygen-containing atmosphere. It is oxygen-stabilized alpha phase — harder, more brittle, and with dramatically reduced fatigue life compared to the bulk material.
Alpha case depth in hot rolling can reach 0.025–0.250 mm depending on:
- Furnace atmosphere (electric vs gas furnace; inert gas vs air)
- Soak temperature and time
- Number of reheats
This contaminated layer must be completely removed by pickling before cold rolling or final use. The HF-HNO₃ pickle dissolves the scale AND the alpha case layer. Inadequate pickling that removes scale but leaves alpha case is a silent quality failure — the material looks clean but the fatigue life may be 30–50% below specification.
Verification: Alpha case depth can be checked by cross-section metallographic examination. Some aerospace specifications (e.g., AMS 4911) include maximum allowable alpha case depth limits.
Prevention in hot rolling:
- Use electric resistance or induction heating with inert atmosphere or vacuum where possible
- Apply anti-oxidation coatings (e.g., water-glass based) before furnace entry
- Minimize furnace soak time (heat quickly, roll promptly)
- Clad rolling of highly reactive alloys (Ti-Al intermetallics, beta alloys) in mild steel packages provides thermal insulation and atmospheric isolation
Common Rolling Defects and Root Causes
Knowing what can go wrong — and why — is often the most practical information an engineer needs. This is what I see come up repeatedly in supplier quality discussions:
| Defect | Most Likely Cause | Corrective Action |
|---|---|---|
| Edge cracking | Temperature too low for alloy; excessive reduction per pass | Increase start temperature; reduce pass reduction to ≤15% |
| Surface scale inclusion | Insufficient pickle before cold rolling; pickle time too short | Verify HF-HNO₃ concentration and immersion time per alloy |
| Wavy edges / center buckle | Crown mismatch between rolls and slab; uneven temperature | Check roll crown; improve furnace temperature uniformity |
| Delamination | Pre-existing billet segregation or porosity; rolled closed | NDT (UT) billet before rolling; verify billet source |
| Work hardening crack in cold rolling | Total cold reduction exceeded limit before anneal | Reduce pass reductions; schedule intermediate anneal sooner |
| Coarse basketweave microstructure | Final rolling done above beta transus | Finish all final passes in (α+β) region; verify temperature measurement |
| Dimensional camber (banana shape) | Top/bottom temperature gradient during rolling; uneven reduction | Improve furnace uniformity; use roller leveler after rolling |
| Alpha case remaining after pickle | Pickle time insufficient; HF concentration depleted | Analyze pickle bath regularly; extend soak time; verify with metallography |
How to Specify: A Decision Framework
The most common question in practice: hot-rolled or cold-rolled for my application?
Choose hot-rolled (Condition A) when:
- Thickness > 3 mm (hot rolling is the only practical option at plate thicknesses)
- Cost is the primary driver and surface finish >1.6 µm Ra is acceptable
- Parts will be machined, not formed — surface waviness doesn’t matter post-machining
- Application is structural or pressure vessel (chemical industry, shipbuilding)
Choose cold-rolled (Condition A or C) when:
- Thickness < 3 mm and especially < 1.5 mm
- Surface finish Ra < 1.6 µm required (biomedical, heat exchangers, consumer)
- Tight dimensional tolerance required (±0.10 mm or better)
- Part involves precision forming where spring-back consistency matters
- Application is foil, shim stock, or thin-wall tube strip
Choose warm-rolled when:
- Thickness 0.5–2.0 mm and the alloy is Ti-3Al-2.5V
- Cost is a factor but HR surface finish is unacceptable
- Intermediate step in a complex cold rolling campaign
Lubrication in Titanium Cold Rolling: What’s Different
Standard mineral oil and sulfurized extreme-pressure lubricants used in steel cold rolling are not suitable for titanium. Sulfur can contaminate the titanium surface and reduce corrosion resistance. High-chlorine lubricants can cause stress corrosion cracking in some titanium alloys under the right conditions.
Acceptable lubricants for titanium cold rolling:
- Synthetic esters (clean-burning, chlorine-free)
- Fatty acid esters (animal or vegetable oil-based)
- Water-based emulsions specifically formulated for titanium (low or no chlorine, no sulfur)
The lubricant must be completely removed before annealing — residual organic lubricant in the anneal furnace contributes carbon contamination. Cleaning is typically done with alkaline degreasing followed by a light acid rinse before the intermediate anneal.
Post-Rolling Heat Treatment Quick Reference
Final properties are set in the annealing step after rolling. For purchasing engineers reviewing certs, here’s what the key conditions look like:
| Alloy | Condition A Anneal Temp | Time | Atmosphere | Tensile (UTS typical) |
|---|---|---|---|---|
| CP Grade 1 | 650–760°C | 30–120 min | Inert or vacuum | ≥240 MPa |
| CP Grade 2 | 650–760°C | 30–120 min | Inert or vacuum | ≥345 MPa |
| CP Grade 4 | 700–790°C | 30–120 min | Inert or vacuum | ≥550 MPa |
| Ti-6Al-4V | 700–845°C | 1–4 hr | Inert or vacuum | ≥895 MPa |
| Ti-3Al-2.5V | 650–760°C | 30–120 min | Inert or vacuum | ≥620 MPa |
Cooling rate matters: CP grades are typically air-cooled from anneal temperature. Ti-6Al-4V is sensitive to cooling rate from the solution temperature when STA condition is specified.
Summary
Titanium rolling is fundamentally a microstructure control exercise. Every temperature, pass reduction, and annealing step either builds or destroys the properties the final part depends on.
The practical takeaways:
- Hot rolling in the (α+β) region (20–200°C below beta transus) produces the best balance of strength, ductility, and fatigue life for most titanium alloys. β-region rolling is for intermediate breakdown only.
- Cold rolling delivers precision and surface finish but requires discipline — 10–20% maximum per pass, intermediate anneal every 30–60% total reduction, and no sulfur-based lubricants.
- Alpha case is not optional to discuss. Any hot-worked titanium part destined for fatigue-critical service needs verified alpha case removal. Pickling removes scale; it may not remove all alpha case without adequate soak time and HF concentration.
- ASTM B265 Condition A annealed is the correct default specification for most engineers. Only move to Condition C if you need the higher yield strength and your forming process can handle reduced elongation.
- Warm rolling fills a real gap — when you need better than hot-rolled surface quality but can’t justify the full cold rolling + multi-anneal campaign.
The choice between hot and cold rolling is rarely arbitrary in practice. It is determined by the target thickness, the alloy, the application’s surface and tolerance requirements, and often by the downstream forming or machining operations. Get that decision right up front, and the downstream problems shrink considerably.